 Английский
 Испанский
 Португальский
 Русский
 Арабский
 Французский
 Немецкий
 Китайский
 Японский
 Корейский


Прецизионные литые детали
Высокоточные литые компоненты, изготовленные с жёсткими допусками из материалов премиум-класса. Идеально для автомобильной отрасли, медицины, электроники, упаковки и промышленности. Доступны разработка пресс-форм, быстрое прототипирование и серийное производство.
Обзор продукта
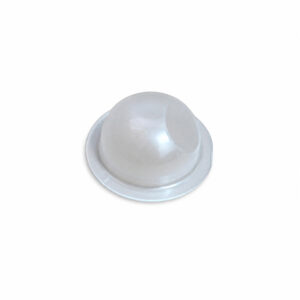
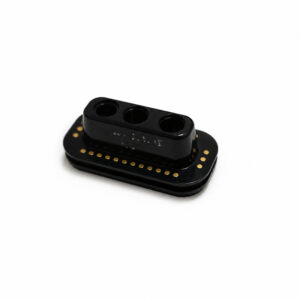
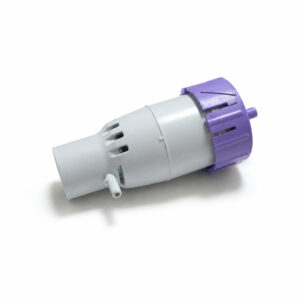
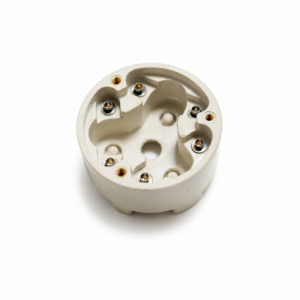
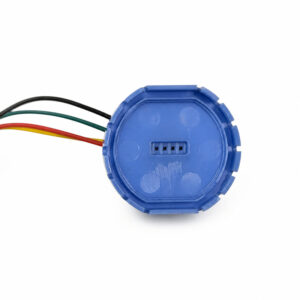
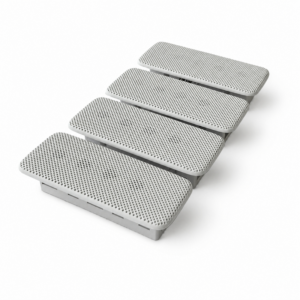
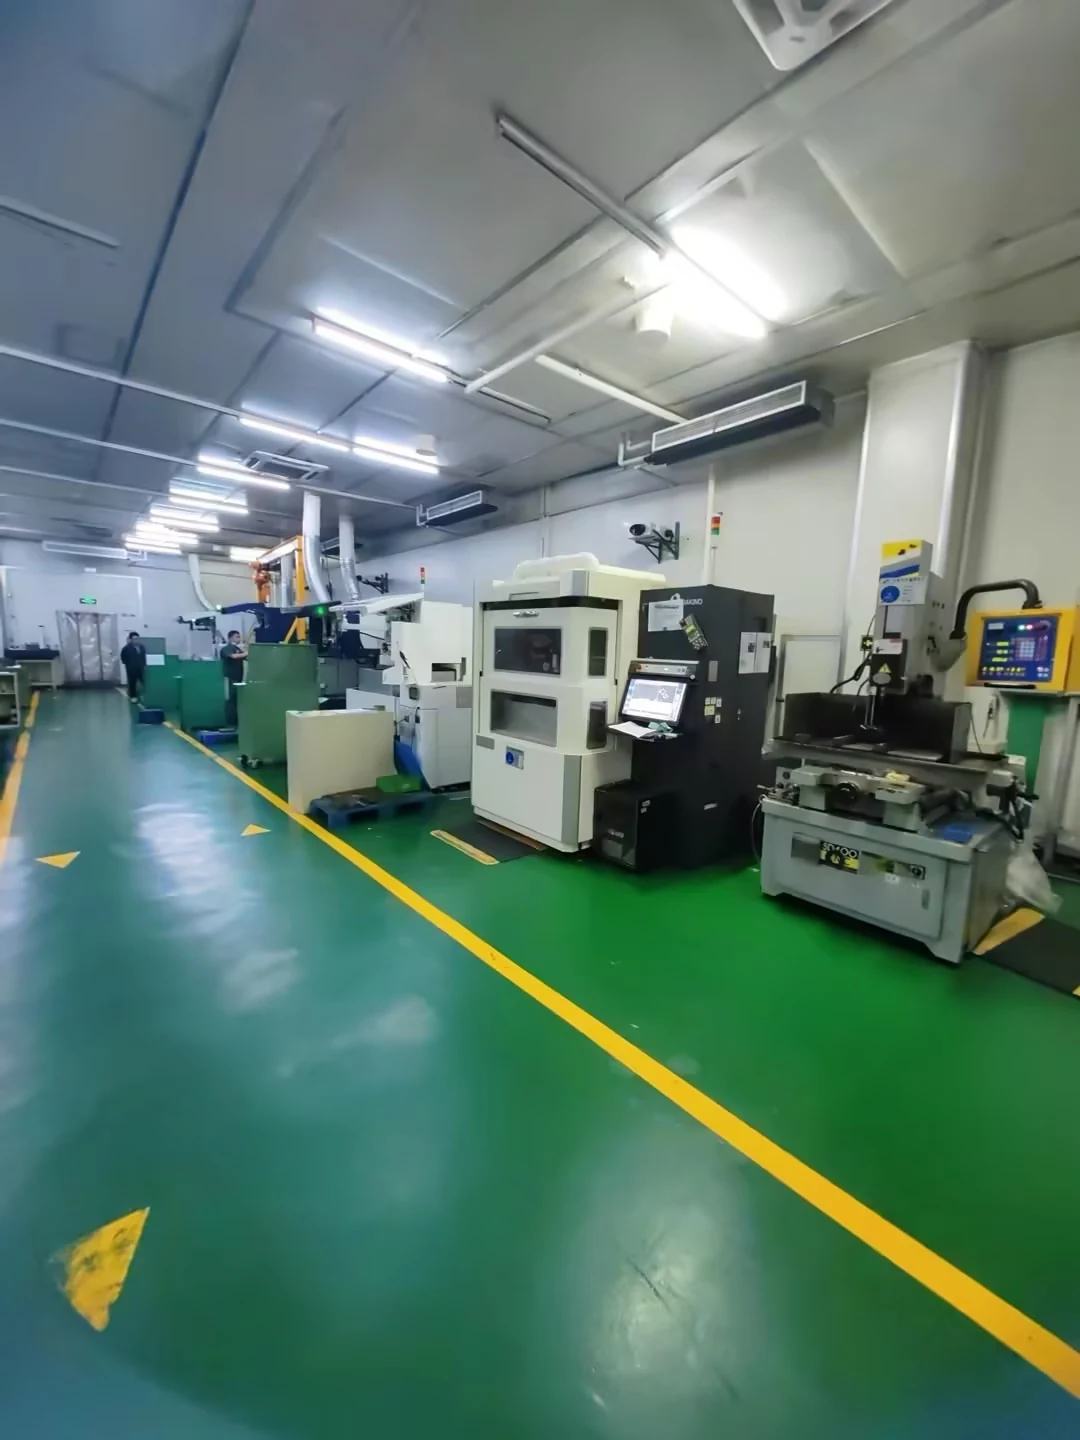
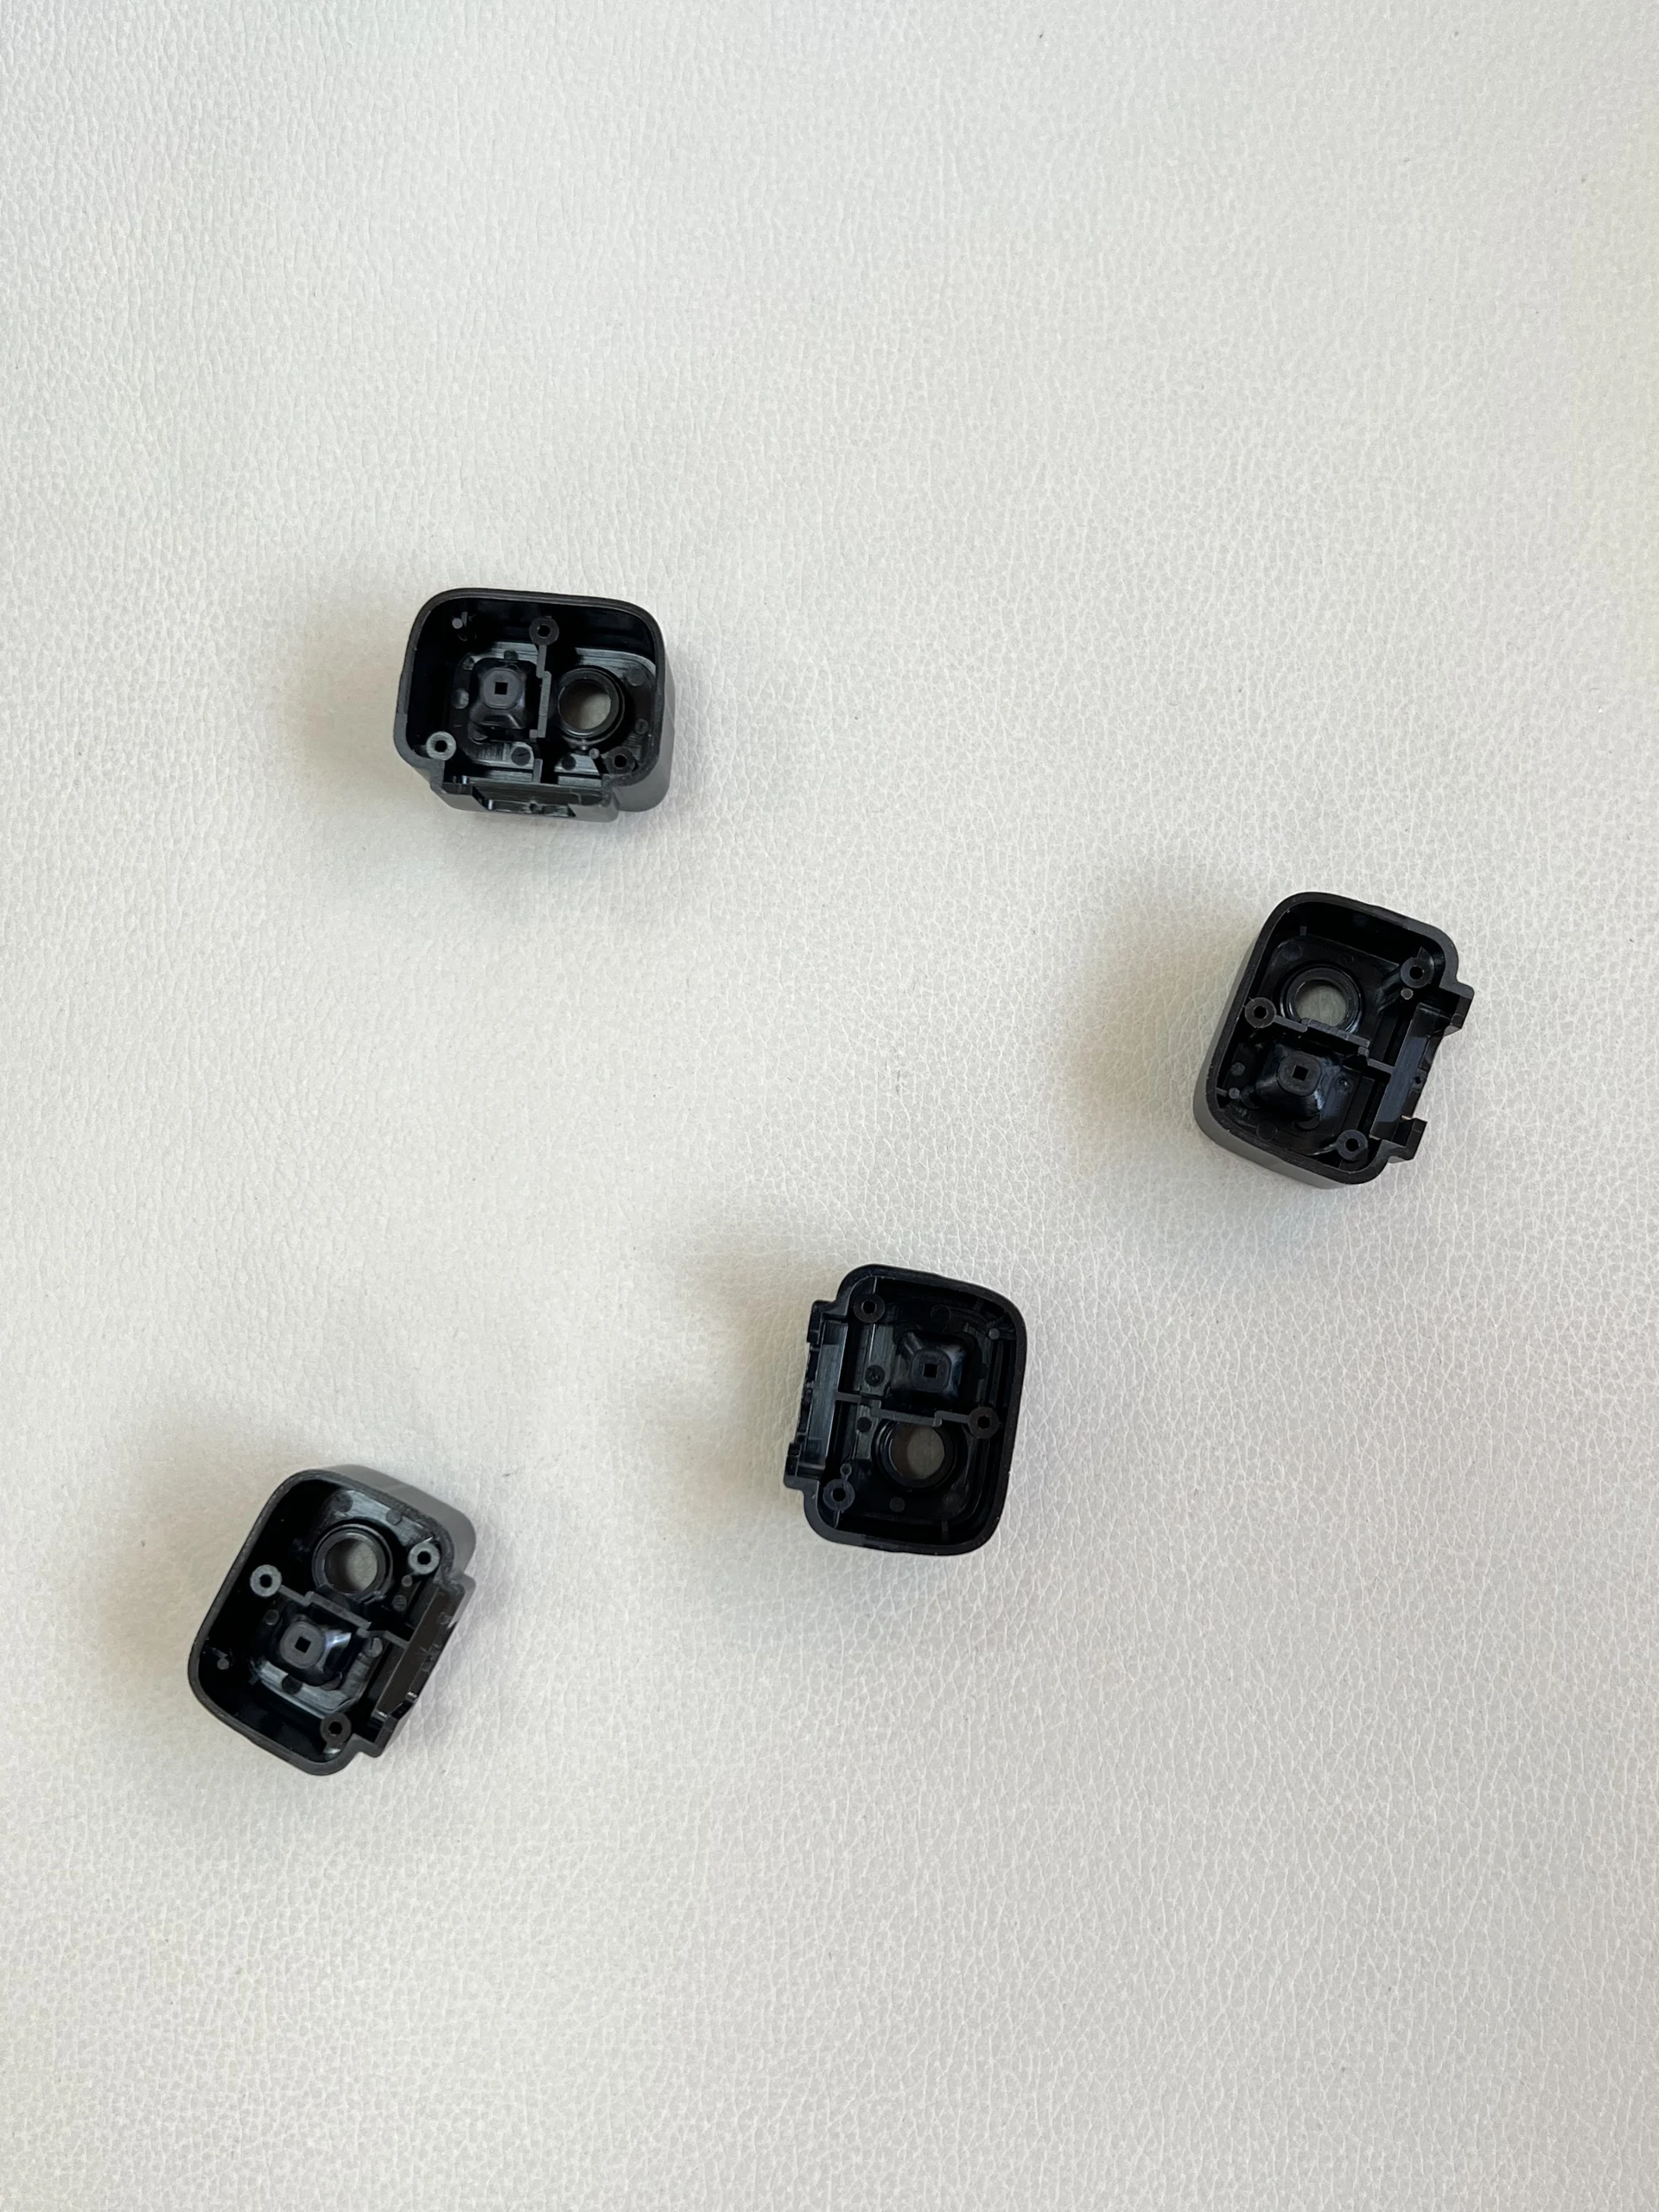
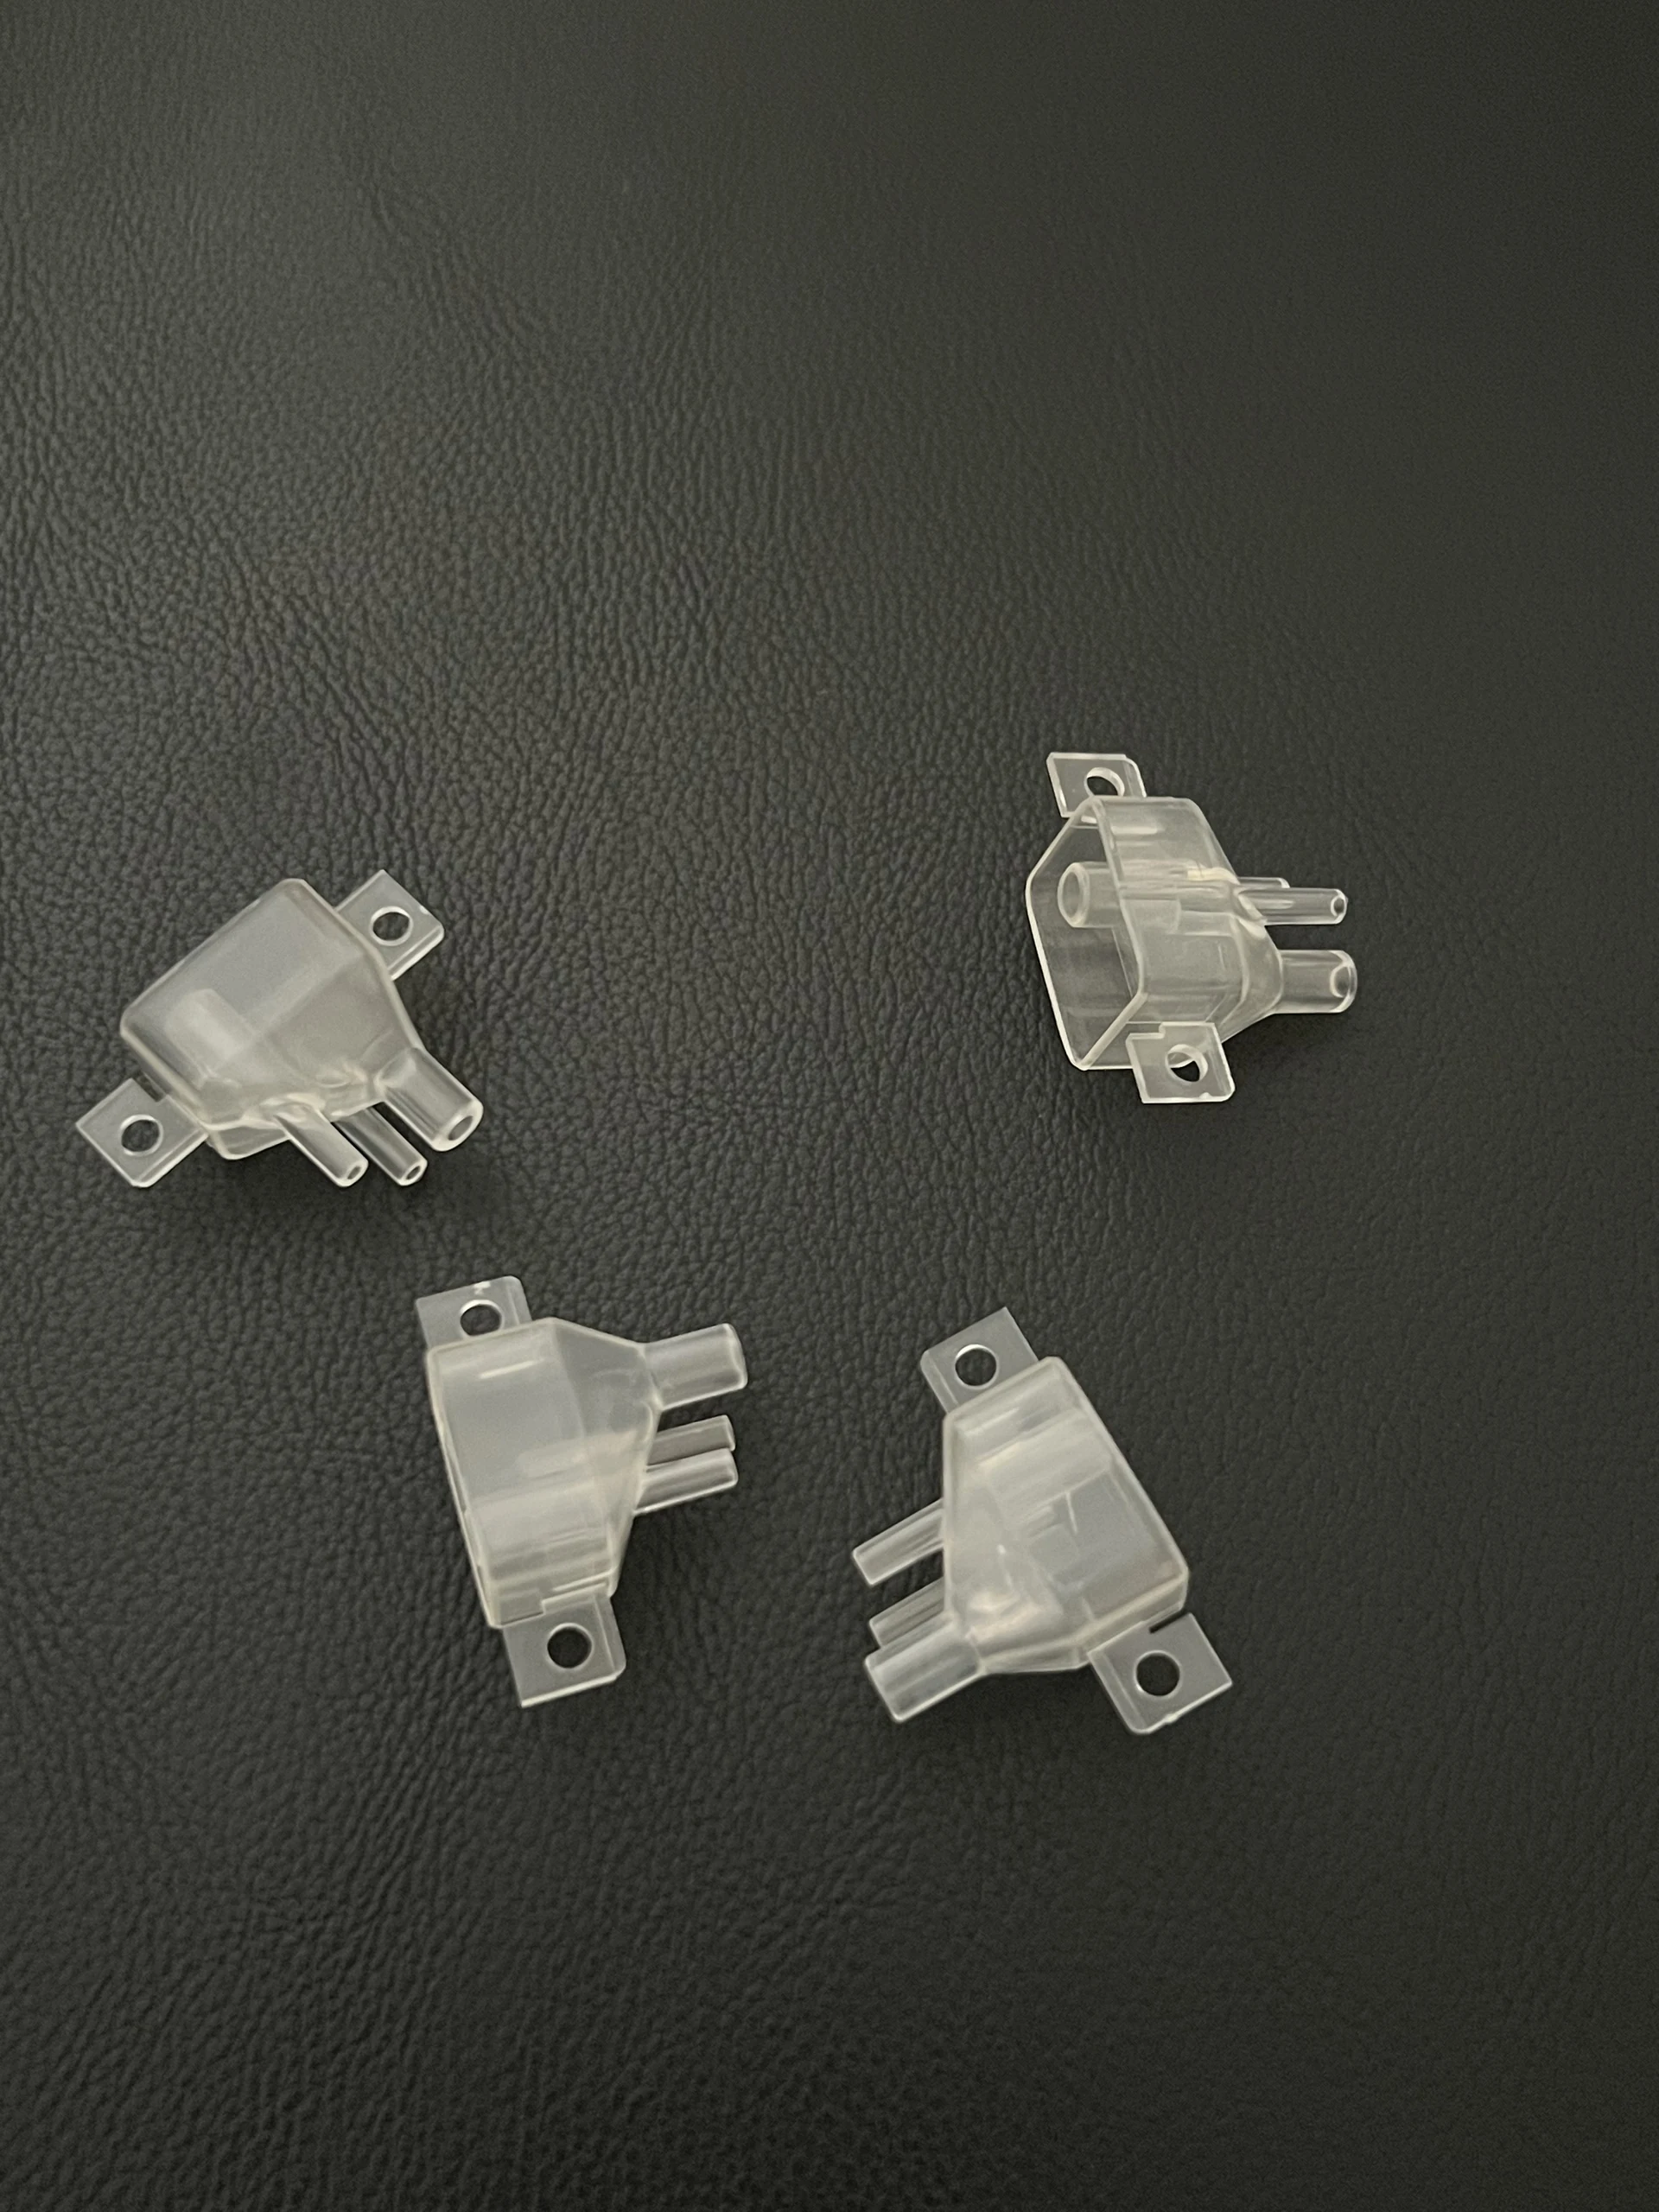
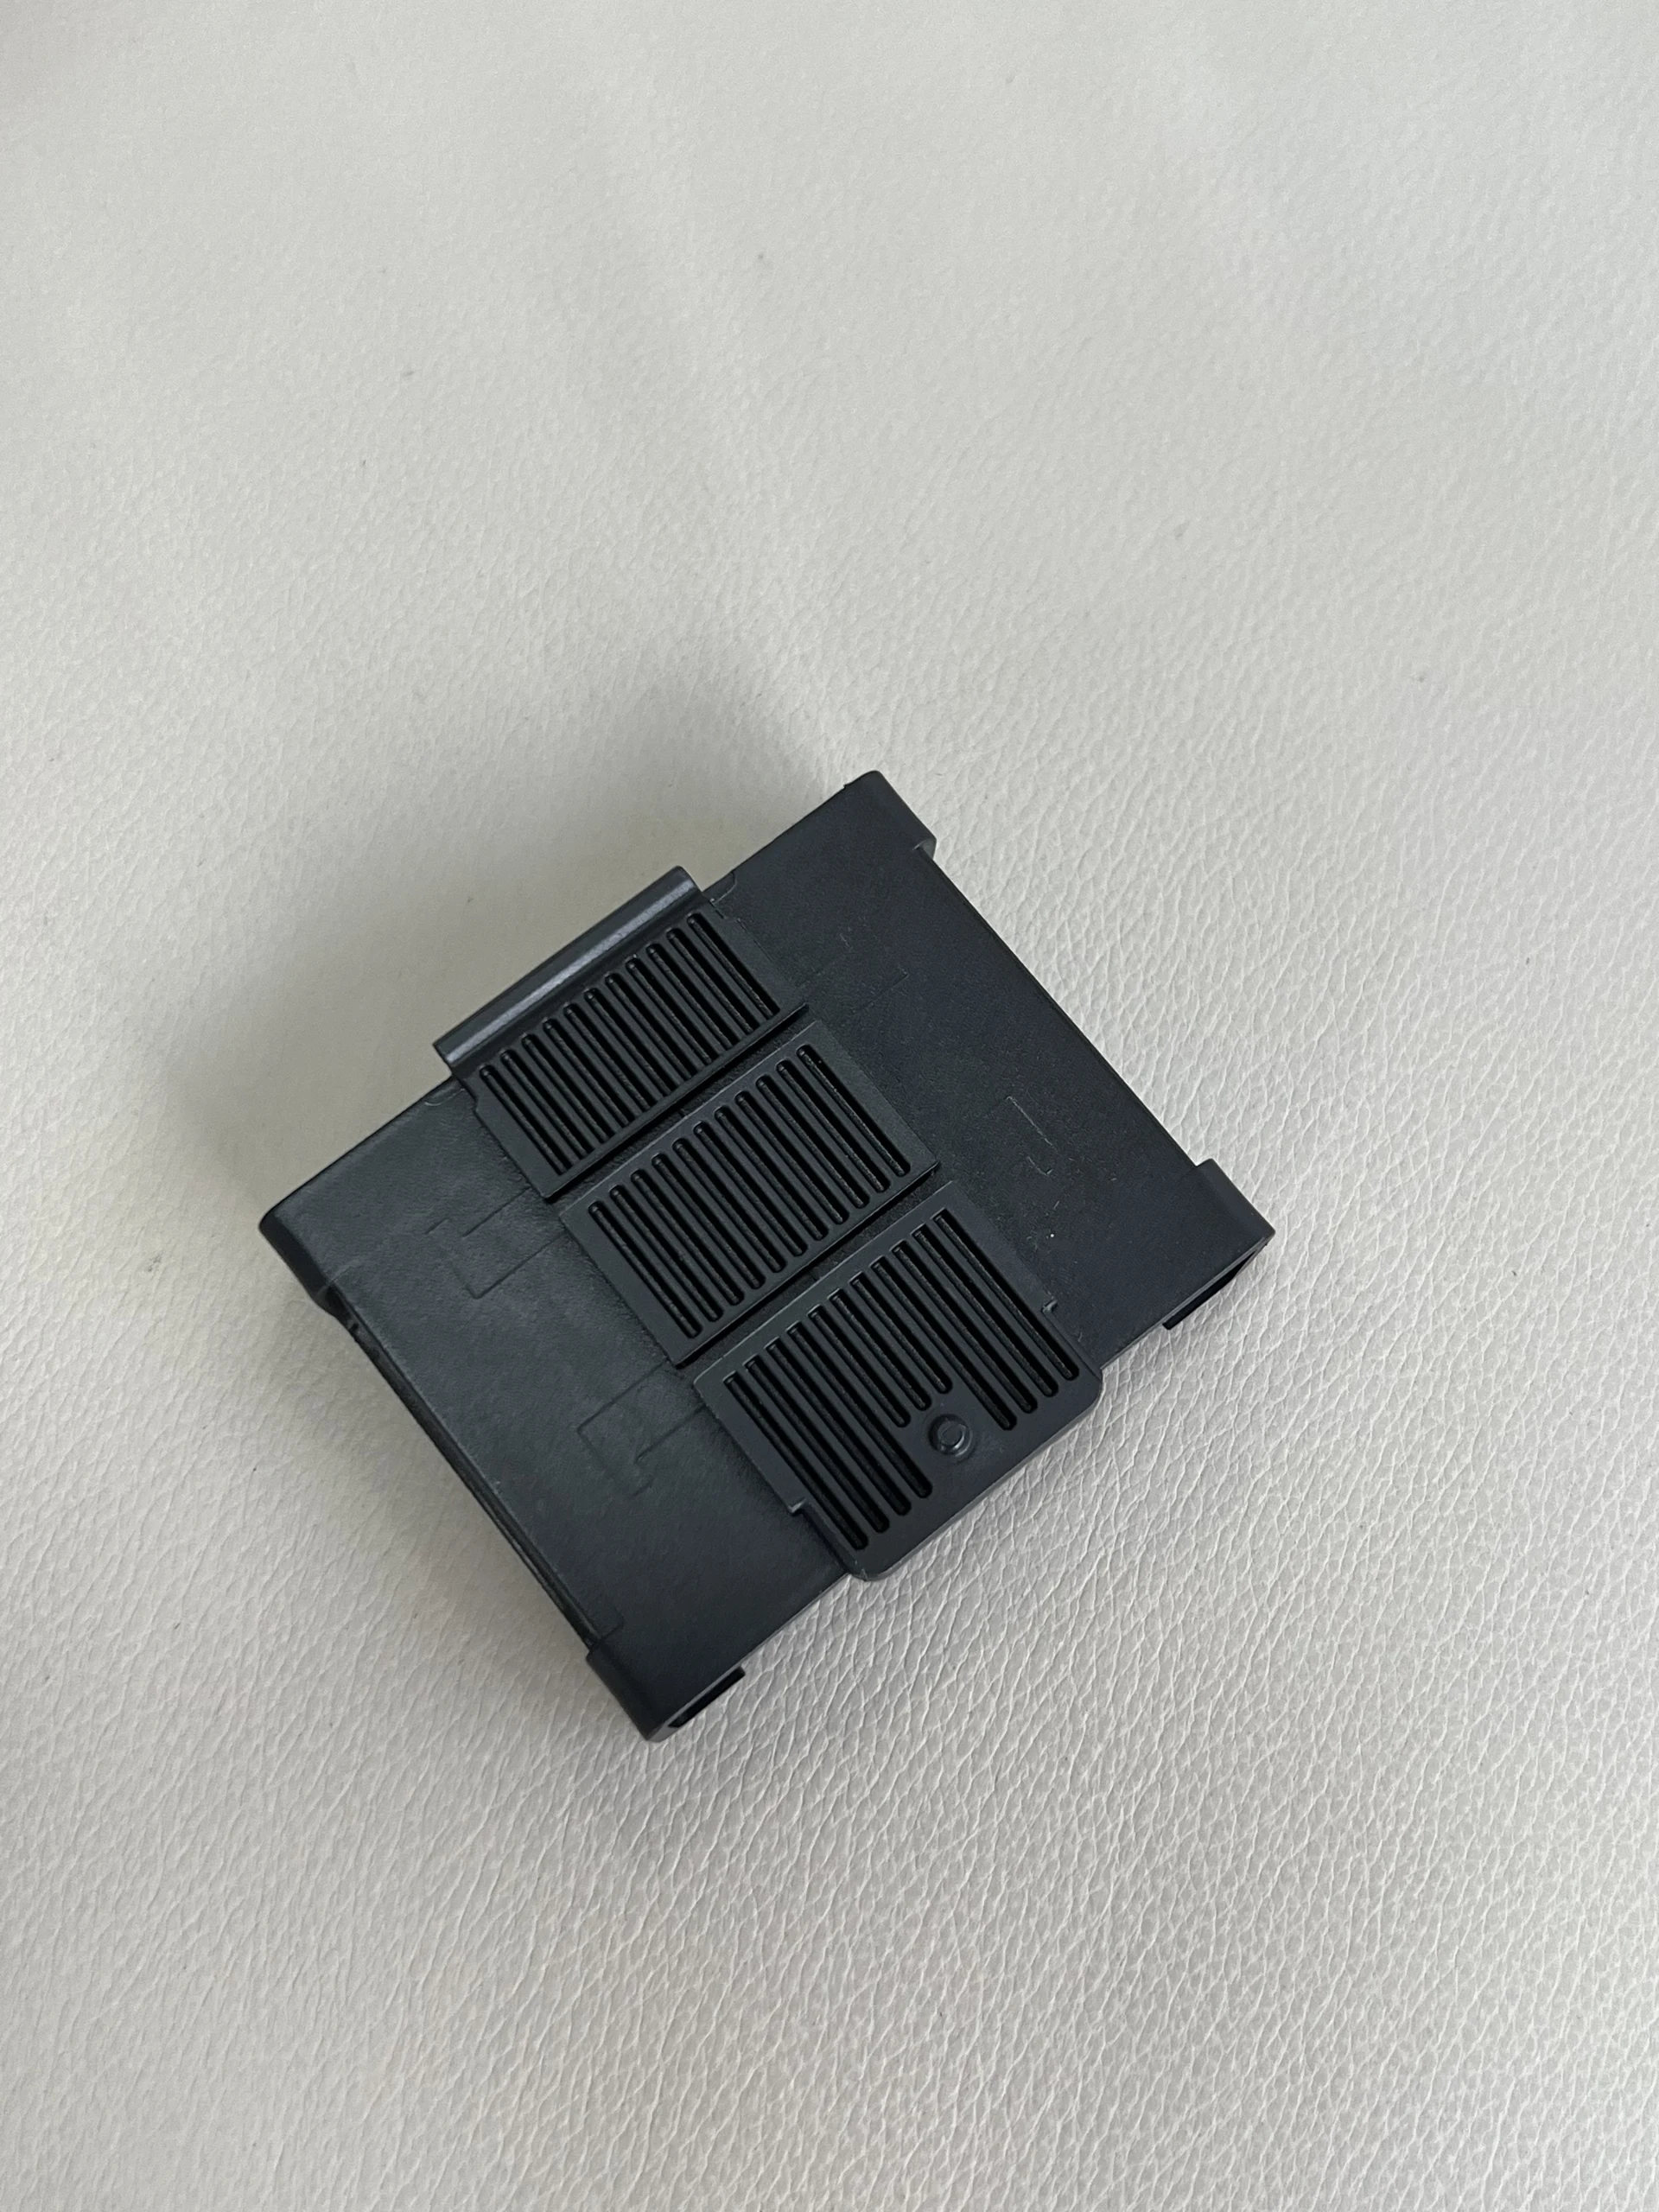
Precision plastic parts vary widely in shape and function, so a useful supply programme starts with a clear engineering brief rather than a generic accuracy claim. JingZhan supports tooling, injection moulding trials and repeat manufacture for custom structural and functional components. The examples below illustrate small moulded parts and ribbed housings; they are not a single standard product with shared dimensions or material. ПРОЕКТИРОВАНИЕ И ПРОИЗВОДСТВО Mark the dimensions that control fit, movement or locating accuracy. Define a datum system and measurement conditions, including any conditioning after moulding. Review the achievable tolerance feature by feature with the resin and geometry, rather than applying the same tight limit everywhere. Review ribs, bosses, corners and thickness changes before tooling. Include suitable draft and radii, and agree where gates and ejectors can be placed. The objective is repeatable geometry with acceptable appearance, not simply a mould that fills once. Provide temperature, load, chemical exposure and appearance requirements. Confirm the exact resin grade, colour and any restrictions on recycled content. Transparent, reinforced or textured parts need different processing and inspection decisions; the sample photographs do not establish those specifications. Inspect first articles against the agreed drawing and test fit with actual counterparts where practical. Record deviations and approved corrections. Выпуск repeat production only when the customer has accepted the relevant dimensional, cosmetic and functional evidence for the defined scope. ТЕХНИЧЕСКИЕ ХАРАКТЕРИСТИКИ ПРОИЗВОДСТВО И ПОВТОРНЫЕ ПОСТАВКИ The supplied manufacturing records include 50–500-tonne injection moulding machines and CNC/EDM tooling resources. Dimensional inspection equipment includes CMM, optical measurement and height measurement. Select a process and inspection route that matches the actual part: the availability of precision equipment does not mean every moulded feature carries the same tolerance or requires the same measurement method. Agree the drawing revision, resin grade, approved samples and critical-to-quality features before release. Record material lots and moulding conditions, inspect first-off parts and use cavity identification where specified. Define packaging, sampling and change approval so later deliveries can be compared with the same baseline. Tool maintenance and replacement inserts should be planned around actual production demand. Инвестиции в оснастку рассчитываются отдельно от цены за штуку. Предоставьте годовой спрос и объемы выпуска, чтобы можно было совместно рассмотреть количество гнезд, закупку и стоимость партии. СМЕЖНЫЕ ПРИМЕНЕНИЯ Structural supports, covers and locating components for electronic and industrial equipment assemblies. Small functional mouldings with openings, ribs, clips or other drawing-defined interfaces. Custom instrument components, including medical-equipment projects when their additional qualification requirements are separately defined. Применение examples indicate possible engineering uses, not approvals or tested performance for every photographed part. Медицина, electrical, flame-rating or chemical-resistance claims require the relevant grade documentation and project-specific validation. Обсудите ваш чертеж и требования к поставке. Отправьте CAD, предпочтения по смоле, критические характеристики, годовую потребность и объем выпуска. Свяжитесь с нашей инженерной командой →Drawing-based precision plastic parts for ongoing supply
Ключевые требования к обработке
Put critical features ahead of blanket tolerances
Design sections for stable filling and cooling
Match resin and finish to the environment
Use trials to resolve assembly questions
Согласованные параметры для вашей детали
Параметр
Спецификация проекта
Manufacturing service
Custom mould development, injection moulding and repeat component supply.
Материалs
Engineering thermoplastics selected against the project specification.
Geometry
Customer CAD and drawings; no common dimensions for pictured examples.
Tolerance
Feature-specific agreement based on geometry, resin and inspection method.
Surface finish
Colour, texture and permissible moulding marks defined by zone.
Tooling
Cavity layout, inserts and expected demand reviewed before quotation.
Inspection
First-article report and agreed batch sampling or gauges.
Packaging
Part protection, quantity per pack and lot identification to customer needs.
Оборудование, срок поставки и планирование заказов
Элемент планирования
Основание для расчёта стоимости
Анализ DFM
Ориентировочно 3–5 рабочих дней после получения полных чертежей и требований.
Новая оснастка
Ориентировочно 4–8 недель до первой пробной отливки после утверждения конструкции пресс-формы и коммерческого релиза; корректировки и валидация заказчиком — дополнительно.
Объемы заказов
Исходная основа для планирования расценок: пробная партия из 500 штук или повторная партия из 1,000 штук на каждый номер детали, смолу и цвет, при условии расценки проекта.
Повторные заказы
Ориентировочный срок 10–15 рабочих дней после подтверждения материалов и производственного слота. Квалификация заказчика, специальная обработка и транспортировка оплачиваются дополнительно.
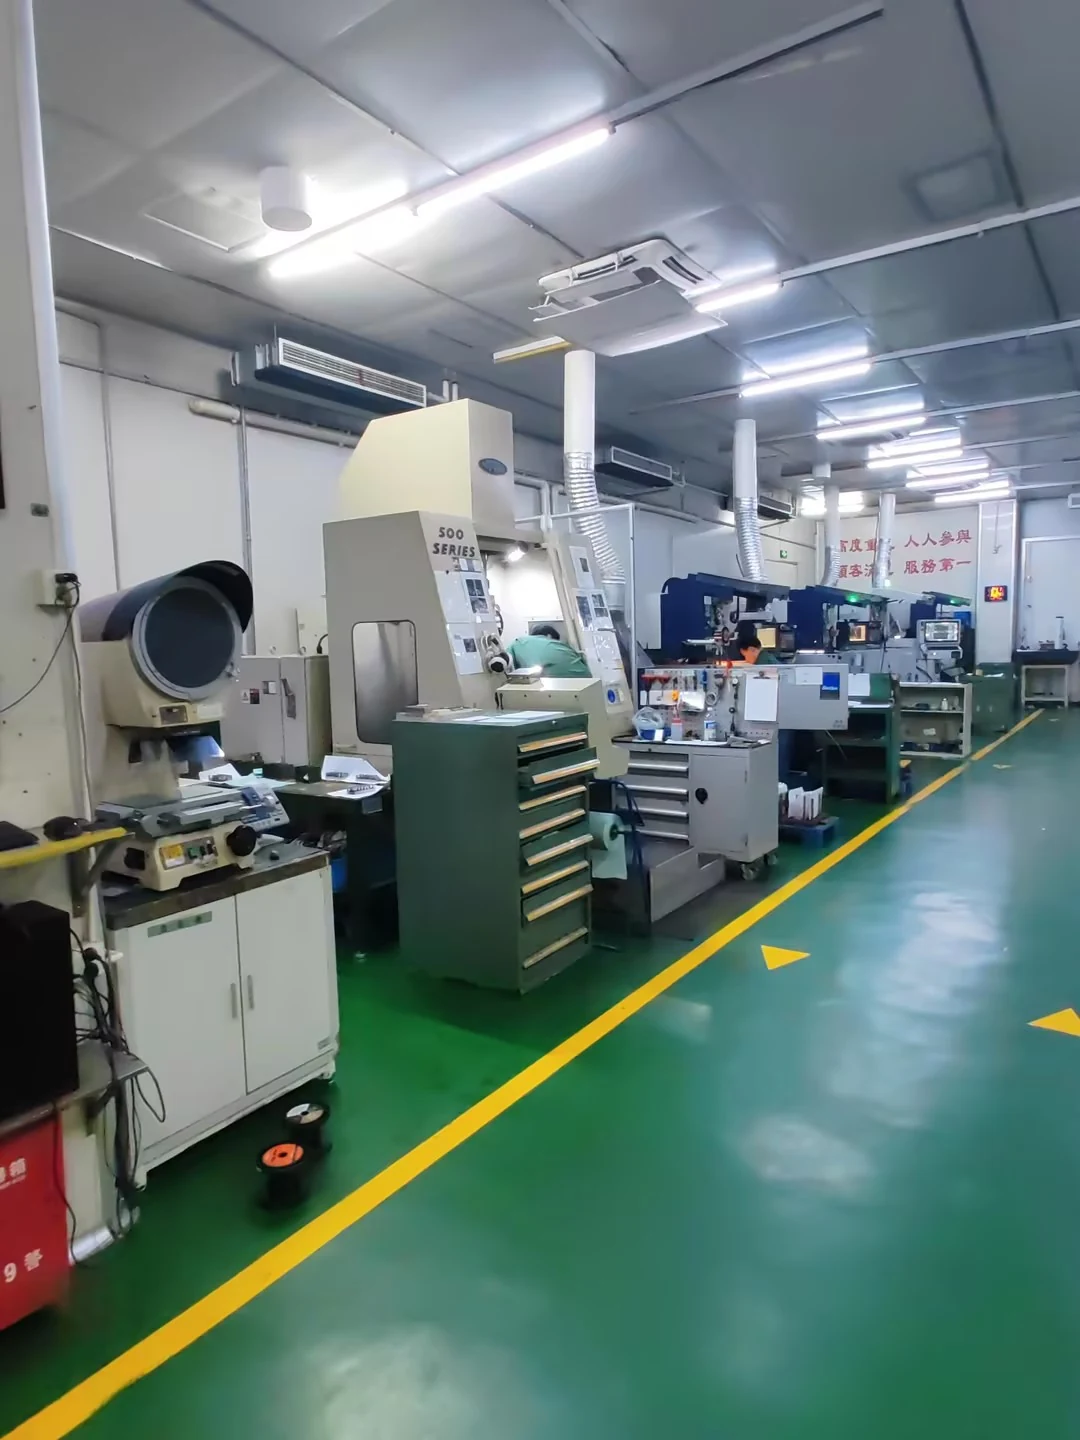
Поддерживайте повторные заказы на утвержденной базовой линии
Где можно использовать эти компоненты
Технические характеристики
Наши возможности литья охватывают широкий спектр материалов, размеров деталей и уровней сложности. Ниже приведены подробные технические параметры.
| Усилие смыкания | 80 1 600 тонн |
| Макс. вес детали | 0,1 г 6 000 г |
| Макс. размеры детали | 1 200 × 800 × 400 мм |
| Давление впрыска | До 2500 бар |
| Материалы пресс-формы | ABS, PC, PP, PA66, POM, PEEK, PMMA, TPE и т. д. |
| Срок службы пресс-формы | 500 000 2 000 000 циклов |
| Срок изготовления | 150 рабочих дней (образец T1) |
| Сертификация | ISO 9001:2015, IATF 16949, ISO 13485 |
| Специальные процессы | Литьё с закладными элементами, овермолдинг, двухкомпонентное литьё |
Рекомендуемые продукты
Ознакомьтесь с нашими высокоточными литыми компонентами, которым доверяют лидеры отрасли по всему миру.